
Top 10 Profile Projectors for Precision Measurement and Quality Control
2026-09-16
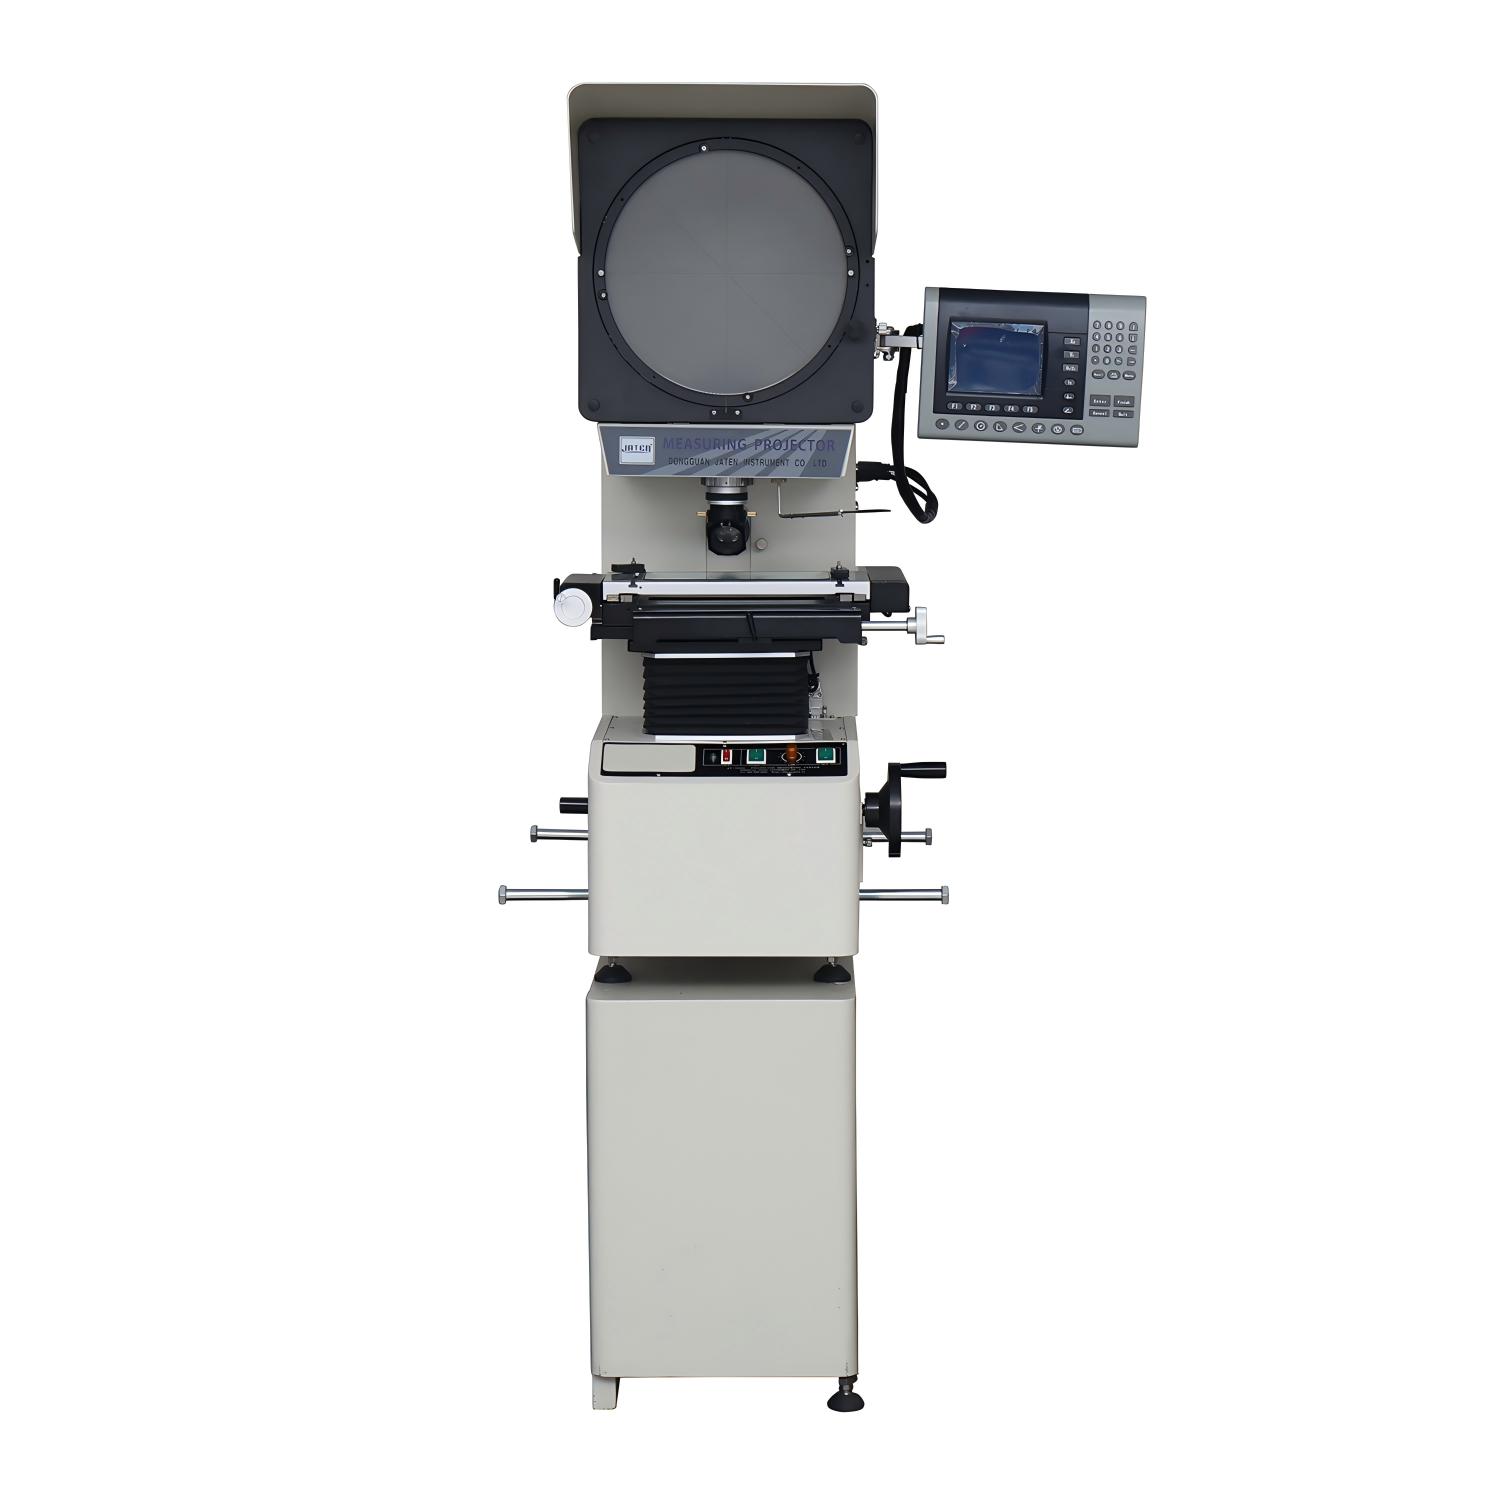
Precision measurement hinges on tools that don’t just promise accuracy—they prove it in every shadow and contour. When quality control demands more than a quick glance, profile projectors step in as the unsung heroes of dimensional inspection. But with so many options flooding the market, how do you separate the workhorses from the impostors? In this roundup, we’ve cut through the noise to spotlight ten machines that truly earn their place on the bench. From optical clarity to stage stability, each pick has been weighed for real-world performance—not just spec-sheet bravado. And if you’re looking for a name that consistently delivers robust engineering without the hype, keep an eye out for JATEN, a brand that quietly checks all the right boxes for demanding QC environments. Ready to see which projectors made the cut? Let’s dive in.
Precision Beyond the Naked Eye: What Sets These Projectors Apart
Most people judge sharpness by pixel count, but the eye glosses over subtle flaws that accumulate into a soft, fatiguing image. These projectors attack those flaws at the optical level. Each lens assembly is aligned and cemented in a dust-controlled environment, then checked for lateral chromatic aberration under a microscope. That means red, green, and blue channels land on the same micro-mirror instead of drifting apart at the screen edges. The result isn't just more detail—it's a cleaner edge, less color bleed, and a picture that holds up when you walk closer.
Thermal expansion is another quiet killer. As a lamp or laser heats the chassis, ordinary optics shift by fractions of a millimeter, enough to blur one corner. Here, the light engine is mounted on a low-expansion chassis and the lens barrel is pre-stressed to stay centered. Factory calibration stores per-unit gamma and color uniformity maps, so the projector you unbox behaves like the reference unit, not a lottery ticket. Even after hundreds of hours, focus stays locked across the whole frame.
From Aerospace to Automotive: Real-World Quality Control Wins
In aerospace, a single microscopic crack can ground a fleet, so inspection routines rely on phased array ultrasonics and laser shearography to catch flaws deep inside composite wings. Those same techniques, when adapted for automotive stamping lines, now flag sub-surface porosity in aluminum door panels before they ever reach a paint booth. The lesson isn't about borrowing tools, but about rethinking failure thresholds: a tolerance that saves a turbine blade doesn't automatically make sense for a suspension knuckle, yet the principle of mapping stress paths remains identical.
Consider how flight-critical fastener torque audits migrated to engine assembly plants. Aerospace demands traceable torque signatures for every bolt, recorded and stored for decades. Automotive teams initially dismissed that as overkill, until warranty data showed that inconsistent clamp loads on battery trays were causing intermittent electrical faults. By adopting the aerospace practice of statistical torque monitoring—not just spot checks but continuous distribution analysis—one EV manufacturer cut warranty claims by a third in eighteen months. The real win wasn't the sensor, but the discipline of treating every joint as a potential failure mode.
What often gets overlooked is the shift in problem-solving culture. Aerospace engineers assume a defect will eventually be found, so they design inspection into the process from day one. Automotive lines, pressed for cycle time, tend to bolt on inspection at the end. When a tier-one supplier began using aerospace-style first-article inspection reports for plastic injection molds, scrap rates dropped even before production started—because the documentation forced designers to confront draft angles and venting issues while the mold was still on the CAD screen, not on the shop floor. That's the real crossover: not the gadget, but the habit of front-loading quality decisions.
Decoding Optics, Stages, and Software: Features That Matter
A microscope’s reputation often rests on its objective lenses, but the real story is in how the whole optical path behaves under daily use. Chromatic aberration, field flatness, and light transmission don’t just sound impressive in a spec sheet — they determine whether you see a faint cellular boundary or miss it entirely. Pay attention to how the optics handle low-light samples and whether the eyepieces stay comfortable during long sessions.
The stage is where frustration either builds or disappears. A rigid stage with smooth, backlash-free movement lets you scan a slide without losing your place, while coarse adjustments that drift can ruin high-magnification work. Look for stages that accept a variety of holders and offer enough travel for your largest samples, not just the standard glass slide.
Software ties the whole experience together, but it should stay out of the way. The best imaging programs give you fast exposure control, reliable stitching for large areas, and measurement tools that don’t require a manual. If the software forces you to export to another program just to annotate an image, it’s already costing you time. Choose interfaces that feel closer to a camera app than a cockpit.
Side-by-Side: How the Top 10 Compare on Key Specs
When you line up the top 10 models on a single spec sheet, the first thing that jumps out is how little separates the leaders from the pack in raw numbers. Battery capacities cluster within a few hundred milliamp-hours, screen sizes hover around the same half-inch band, and processor clock speeds differ by a rounding error. What actually shifts the ranking is the tuning: two phones can share the same sensor but produce wildly different photos because one leans on aggressive computational sharpening while the other lets noise live for a more film-like grain. That's the gap you won't see in a checkbox comparison.
Build materials tell a similar story. Nearly every flagship now claims a glass sandwich and an aluminum frame, yet the hand-feel varies from slippery and premium to grippy and almost rubberized. Weight distribution matters more than total mass; a 210-gram phone balanced low in the chassis feels lighter than a 195-gram one that's top-heavy. The spec sheet says "stereo speakers," but one device pumps out tinny highs while another delivers a surprisingly wide soundstage. These are the details that separate a device you tolerate from one you reach for without thinking.
Perhaps the most misleading column is fast charging. A 120W brick sounds twice as fast as 60W, but sustained charging curves tell the truth: some phones hold peak speed for only four minutes before throttling, while others cruise at 45W for half an hour and finish nearly as quickly. Real-world endurance under mixed use rarely matches lab numbers either. So instead of crowning a winner by the longest spec bar, we look at how each phone behaves when you're down to 15% battery at 6 p.m. and still need navigation home.
Setup Smarts: Getting the Most Accurate Measurements Fast
Before you even pick up a tape measure, scan the room for the flattest, most stable surface you can find. A slight tilt or uneven floor will throw off your numbers more than any tired eyes ever could. If you're working outdoors, take an extra thirty seconds to stomp down loose soil or clear away gravel—small shifts underfoot often translate into measurement drift that only shows up after you've already cut or mounted something.
Instead of relying on the cheap hook at the end of your tape, start from a fixed reference point like a door jamb, a cabinet edge, or a clamped straightedge. For longer spans, use a laser measure but bounce it off a solid target—plain paper can scatter the beam and give you a false reading. When you need to repeat a measurement, don't trust your memory: jot down the first number, remeasure from the opposite direction, and compare. The difference between the two is usually the true error in your setup, not in the tool.
Speed comes from eliminating rework, not from rushing the initial reading. Set your tool down, take a breath, and sight along the markings at eye level rather than from an angle. For tapes, pull just enough tension to remove sag, but don't stretch the blade—too many people yank it tight and then wonder why their shelf is an eighth of an inch short. A two-second pause here saves you a trip back to the saw.
Future-Proofing Your Inspection Line: Trends in Projector Tech
Projector technology for inspection lines has quietly shifted from a replaceable commodity to a strategic asset. The old habit of buying the brightest lamp-based unit and calling it a day no longer holds. Today, the conversation centers on how illumination geometry, spectral stability, and onboard processing can bend the cost curve over a decade of operation. Teams that treat projection as a fixed cost get surprised by drift, heat fade, and obsolete lamp inventories. Teams that treat it as a controllable variable start asking different questions: how does the projector behave at hour 40,000, not hour 40?
One under-discussed trend is the move away from raw lumen wars toward contrast fidelity under factory lighting. Inspection lines rarely run in darkrooms. Stray reflections from polished metal, glossy packaging, or oily surfaces punish any projector that cannot hold a tight black level. Solid-state illumination—LED and laser-phosphor—has matured enough that color separation and grayscale tracking stay predictable across shifts, but the real differentiator is how manufacturers handle thermal load. A projector that throttles its output by 15% after three hours will silently corrupt pass/fail thresholds. Future-proof lines are specifying not just brightness but sustained brightness over an eight-hour thermal cycle, with logged output curves instead of marketing spec sheets.
The third shift is less about optics and more about integration. Inspection projectors are becoming edge devices. Onboard pattern memory, industrial Ethernet control, and health telemetry now matter as much as lens quality. A line that can push a new calibration pattern to twenty projectors in under a minute, or receive an alert before a color channel degrades past tolerance, avoids the classic scenario where a subtle failure goes unnoticed until a customer rejects a full batch. The future-proof line treats its projectors as a network of measurement instruments, not a row of dumb light boxes. That means ditching proprietary control software, asking for REST or OPC-UA interfaces, and budgeting for periodic spectral verification instead of reactive bulb swaps.
FAQ
Start with the optical system. A telecentric lens and a well-corrected projection lens keep edges sharp across the entire screen, which matters more than raw magnification. Then check the stage travel, resolution, and repeatability, especially if you plan to measure parts with multiple datums. Don't overlook the light source either; a halogen or LED profile illuminator with adjustable intensity gives you better contrast on tricky edges.
A profile projector gives you a real optical image on a screen, which is great for quick visual comparisons, overlays, and operator training. Vision systems rely on cameras and software, so they offer automated edge detection and data logging but need more setup and maintenance. For mixed lots or one-off inspections, many shops still prefer the immediate feedback of a projector, especially when tolerances are in the ±0.001 inch range.
You'll find them heavily used in machining, automotive, aerospace, and medical device manufacturing. Any place that produces turned, milled, stamped, or injection-molded parts with critical profiles can use one. Tool and die shops also keep them handy for checking cutting edges, radii, and thread forms without sending parts to a lab.
Profile lighting, or transmitted light, is usually the default because it creates a silhouette that's easy to compare against a drawing or overlay. Surface lighting helps when you need to see surface details, blind holes, or recessed features. Many top-rated projectors let you blend both types or switch between them quickly, which is essential when inspecting parts with both external and internal geometries.
Most standard profile projectors are designed for 2D measurements, but you can measure some vertical features by using a focusing method or a touch probe accessory. However, those measurements are usually less accurate than using a dedicated height gauge or CMM. If you regularly need step heights or depths, consider a model with a Z-axis scale and a probe option, or pair the projector with a separate height measurement tool.
Calibration frequency depends on usage and environment, but a good rule is every six to twelve months for production environments. The process typically involves checking magnification accuracy with a glass scale or stage micrometer, verifying stage travel in both axes, and confirming that the screen center and crosshairs align with the optical axis. Any certified lab can do this, though many facilities train in-house metrology staff for routine checks.
Names like Mitutoyo, Starrett, Nikon, and OGP (Optical Gaging Products) have strong reputations for build quality and optical performance. Lesser-known but still capable options include J&L Metrology and Dorsey Metrology for specialized or budget-conscious needs. The right choice depends less on brand prestige and more on screen size, stage capacity, and whether you need digital readouts or software integration.
One big mistake is using the wrong magnification for the tolerance band; too much magnification can make edges look fuzzy and exaggerate minor irregularities. Another is ignoring stage cleanliness or failing to zero the digital readout before a session, which leads to systematic errors. Also, many operators rely too heavily on the screen image and forget to verify with a physical overlay or template, especially for critical dimensions.
Conclusion
For any shop floor where precision measurement is non-negotiable, these ten profile projectors genuinely close the gap between what the naked eye misses and what a quality standard demands. They have earned their place in aerospace and automotive inspections—think turbine blade contours or injection-molded part flash—where a few microns decide pass or fail. What separates the leaders isn't just optical clarity but how well their stages, lenses, and measurement software work together under real lighting conditions. A side-by-side look at working distance, screen size, and digital readout accuracy reveals that one model might excel on large, heavy parts while another wins on repeatable edge detection for tiny features. Buyers do well to ignore marketing gloss and instead test each unit with their own sample parts, because the best projector on paper can still disappoint if its focusing mechanism feels sloppy or its software menus bury common functions.
Beyond the hardware, measurement speed and long-term reliability often hinge on setup habits that are rarely mentioned in manuals. Warming up the light source, verifying magnification with a traceable glass scale, and keeping the stage clean from cutting fluid residue matter more than most users expect. The current wave of projectors is also shifting toward automated edge recognition and direct CAD overlay, so operators spend less time manually aligning crosshairs and more time interpreting data. That trend matters when planning an inspection line: a machine with modest software upgrade paths today can stay relevant three years from now, while a closed, purely optical system may force an expensive replacement. In short, the top ten are not just tools for measurement—they are decisions about how your quality control will adapt as tolerances tighten and parts become more complex.
Contact Us
Contact Person: Volien
Email: [email protected]
Tel/WhatsApp: +86 18029161762
Website: https://www.jatentech.com/