
Slip Ring Manufacturer: Key Factors for Selecting a Reliable Partner for Rotating Connections
2026-10-06
When your rotating systems demand uninterrupted power and data transfer, the choice of slip ring manufacturer can make or break performance. MOFLON stands out by focusing on the details that matter most—durability, customization, and consistent quality. In this guide, we’ll explore the key factors to evaluate so you can select a partner that keeps your operations turning smoothly.
Engineering Depth That Shows Up in the Details
The difference between a good product and a great one often hides in the gaps that most people never see. It’s not about adding more features or chasing the latest trend—it’s about returning to the same edge case for the fourth time because the cursor jumps one pixel when switching between input modes. That kind of persistence rarely makes it into a launch announcement, but it defines how the tool feels after three months of daily use.
Real engineering depth means anticipating what happens when the network drops mid-sync, when a filename contains an emoji, or when a user changes their system clock. These aren’t hypothetical scenarios—they’re the silent majority of real-world usage. Treating them as first-class problems, rather than deferred exceptions, separates software that merely works in demos from software that holds up under the weight of messy, unpredictable everyday life.
The mark of this depth is rarely a single breakthrough. It’s a collection of small, deliberate choices: the exact debounce timing on a search field, the precedence rules for conflicting keyboard shortcuts, the way error messages recover instead of blame. Each choice alone feels minor. Together, they create a quiet competence that users may never consciously notice, but would immediately miss if it were gone.
Custom Designs Without the Custom Headaches
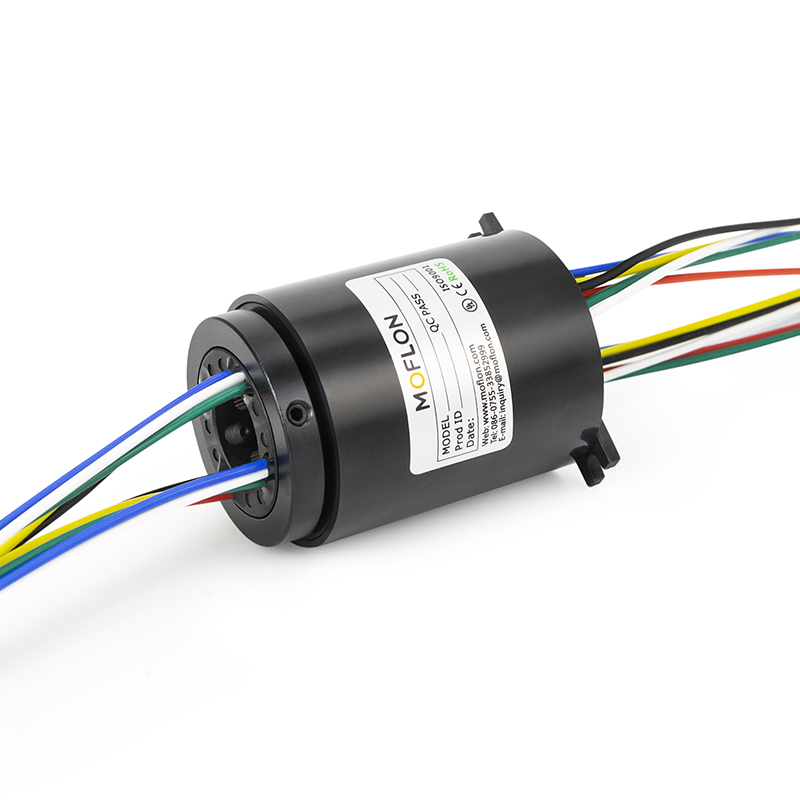
Custom design projects usually drag on for weeks, with endless email threads and surprise invoices. But it doesn't have to be that way. You can get a design that feels made just for you without the usual back-and-forth.
The trick is starting with a flexible foundation instead of a blank canvas. Pick a layout that already works, then swap in your own colors, fonts, imagery, and copy. Because the core structure is solid, changes happen instantly and you never wait on a designer to tweak a button.
The end result is a site or product that looks bespoke but launches in days, not months. No fuss, no delays, no bloated budget—just a custom look without the custom headaches.
Contact Materials That Outlast the Hype
Most contact material datasheets lead with impressive lab numbers—low contact resistance, high hardness, generous mating cycles. Yet field failures often start long before those figures suggest. A material that genuinely outlasts the hype has been punished in ways that matter: fretting under vibration, exposure to mixed corrosive gases, repeated thermal swings with actual connector geometry. Polished coupon tests don't predict connector life; cycling and micro-motion do.
The difference shows up in details. Ask for data from mixed flowing gas tests, not just salt spray. Look at fretting corrosion under load, because that's what kills real contacts in automotive and industrial settings. A contact that survives 10,000 clean-room cycles can pit and oxidize after a few hundred cycles with humidity, dust, and mating misalignment. Materials that last have usually been proven in harsh, dirty, thermally unstable environments, not just on a benchtop.
Longevity also comes from boring histories. The alloys and platings that truly outlast the hype tend to have decades of teardown analysis from underhood connectors, outdoor telecom boxes, or robotic end effectors. Their field return rates are low, and their failure modes are well understood. If a supplier can't show you failed parts from real deployments, the impressive graph on page two is probably just that—a graph.
Testing Protocols That Predict Real-World Wear
The friction between a standardized abrasion machine and an actual jacket sleeve tells two very different stories. While a Martindale or Wyzenbeek test can run thousands of cycles in a climate-controlled room, it cannot reproduce the uneven pressure of elbows on desks, UV exposure from sun, or the slow chemical assault of sweat and body oils. That's why field correlation studies often reveal that a fabric passing 50,000 Wyzenbeek double rubs may still fail at the cuff after eight months of daily use. Smart manufacturers treat lab results as a baseline, then layer in targeted protocols—flex fatigue, crocking, pilling, seam slippage—to approximate the specific stress points of the end product.
One common mistake is reading a single wear metric as the whole story. For upholstery, ASTM D4157 (Wyzenbeek) gives a number for surface abrasion, but it says nothing about how the fabric will behave when repeatedly stretched over a foam edge or exposed to sunscreen on a beach chair. Similarly, ISO 12947 Martindale abrasion is useful for flat textiles, yet it doesn't capture the abrasive bite of concrete or asphalt that flooring and luggage materials often face. The better protocol maps each real-world failure mode—edge wear, seam opening, color transfer, dimensional change—to a specific lab method, and then weighs the results based on how often each failure actually occurs in the field.
Some of the most predictive protocols are intentionally rough and unglamorous. The Taber abraser with CS-10 wheels, for example, is a blunt instrument compared to the subtle wear of a leather steering wheel, but when combined with a humidity soak and a cold flex test, its readings start to align with warranty claims. In practice, companies that run parallel testing—lab abrasion plus a 30-day pilot with employees using the product in real conditions—get the most reliable signal. That hybrid approach uses the lab numbers to sort materials quickly, then lets real-world feedback correct for the blind spots that no standardized test can anticipate.
Support That Extends Past the Purchase Order
A purchase order only starts the clock. Once your equipment arrives, the same technician who ran the pre-ship checklist picks up the phone when you call about a software mismatch, a bent rail from freight, or a torque setting that doesn't match the spec sheet. You're not routed through a portal or handed a ticket number. You talk to the person who already knows your machine's serial number by heart.
That support doesn't fade after the warranty date. We log every service call and follow up on parts that show early wear, sometimes shipping a replacement before you've filed a request. Need a bracket discontinued three years ago, or a modified mounting plate for a conveyor we didn't supply? The small-batch machine shop down the hall from our assembly line keeps those odd jobs moving, usually within the week.
Proof in the Field, Not Just on Paper
Walk through any workshop floor or job site where the tools are actually put to work, and you'll notice a quiet distinction between what's advertised and what's trusted. Engineers can talk all day about torque curves, load ratings, and material grades, but the moment a socket slips under real stress or a wrench rounds off a stubborn bolt, the paperwork loses its authority. The field has its own grading system, one built on sweat, repetition, and the occasional bruised knuckle. That's where reputations are earned — not in a lab report, but in the hands of someone who has to finish the job before sundown.
The difference shows up in small, telling ways. A tool that feels balanced on the third hour of overhead work, a finish that doesn't flake after months in a damp truck bed, a ratchet that still clicks cleanly after being dropped onto concrete more times than anyone can count. These are the qualities you can't measure from a spec sheet. They emerge from use, from failure, from the unglamorous grind of daily work. Ask a veteran mechanic which brand they actually reach for, and the answer rarely matches the top of a buyer's guide. It matches what survived last winter's outdoor teardown or the forty-seventh rusty exhaust flange.
None of this means documentation is worthless — tolerances and certifications have their place. But they are starting points, not proof. Proof lives in the accumulated evidence of real tasks: the transmission pulled in a gravel driveway, the pipe fitting tightened in a crawl space with no room to swing, the hinge adjusted on a gate that freezes shut every January. Until a tool has been tested by that kind of honest, unscripted work, its credentials remain theoretical. The field doesn't care about your brochure. It cares whether the thing works when it matters.
FAQ
Look beyond the sales pitch. Ask for documented life test data under your specific load and speed conditions, not just a generic MTBF figure. Check how they handle signal noise—request an oscilloscope trace from a recent similar project. A reliable partner will also walk you through their failure analysis process instead of hiding behind warranty fine print.
Focus on contact resistance stability across the entire rotation range, insulation resistance at operating temperature, and allowable current density per ring. For data and signal channels, bandwidth and crosstalk isolation are often more critical than the headline voltage rating. If the environment has dust or moisture, the IP rating and venting design should be confirmed with test reports.
It's often the deciding factor. Standard catalog units rarely fit the exact bore size, mounting flange, or mixed power/signal/fiber requirements of real systems. A good manufacturer will offer modular designs and be willing to adjust brush pressure, ring spacing, and housing materials without treating every change as a new engineering project.
Ask how brush replacement is done in the field—can your own technicians do it, or does it require factory service? Request the recommended inspection interval for your duty cycle and the availability of spare ring/brush assemblies. Also clarify lead times for replacement parts, not just complete units, because that often reveals the true after-sales commitment.
Request detailed material datasheets for the contact pairs. Precious metal alloys like gold-on-gold are common for low-current signals, while silver graphite or silver nickel may suit higher power. Be wary of vague terms like "high-quality copper"—ask for specific alloy grades, plating thicknesses, and the manufacturer's wear rate data under your expected current and speed.
They can be a useful baseline, but don't stop there. ISO 9001 says little about electromechanical competence. More relevant are industry-specific approvals like UL, CE, or ATEX if you're in hazardous areas. Ask whether the manufacturer has passed vibration and shock testing to standards your system requires, and request the actual test reports rather than a certificate number alone.
Don't optimize only for initial price. Under-specified rings lead to noise, intermittent connections, and early brush wear that cost far more later. Request a sample or prototype for your exact application, test it for at least a few hundred hours under real load, and compare the measured contact resistance drift. Also check how the manufacturer handles late-stage design changes—flexibility there often indicates better engineering depth.
Conclusion
Selecting a slip ring manufacturer goes beyond comparing catalogs. The real differentiator emerges in engineering depth—small design choices like brush pressure, contact geometry, and housing tolerances determine long-term stability. A reliable partner handles custom requirements without turning them into a drawn-out ordeal, offering modified lead wires, integrated encoders, or non-standard bore sizes as routine work. They also avoid marketing-driven material claims, instead using proven contact systems such as gold-on-gold or fiber brushes that maintain low electrical noise over millions of revolutions.
Testing protocols are where many suppliers cut corners, but a trustworthy manufacturer runs accelerated life tests simulating temperature swings, vibration, and duty cycles to predict actual field wear. Post-sale support matters equally—responsive engineering assistance, spare part availability, and failure analysis after delivery indicate a long-term mindset. Finally, insist on field references from similar applications: wind turbines, medical robots, or packaging lines. Performance data from real installations carries more weight than glossy datasheets.
Contact Us
Contact Person: Xiangpin Li
Email: [email protected]
Tel/WhatsApp: 86 186 1706 8578
Website: https://www.moflon.com