
PE Pipe Machine Factory Innovations for High-Quality Production
2026-09-18
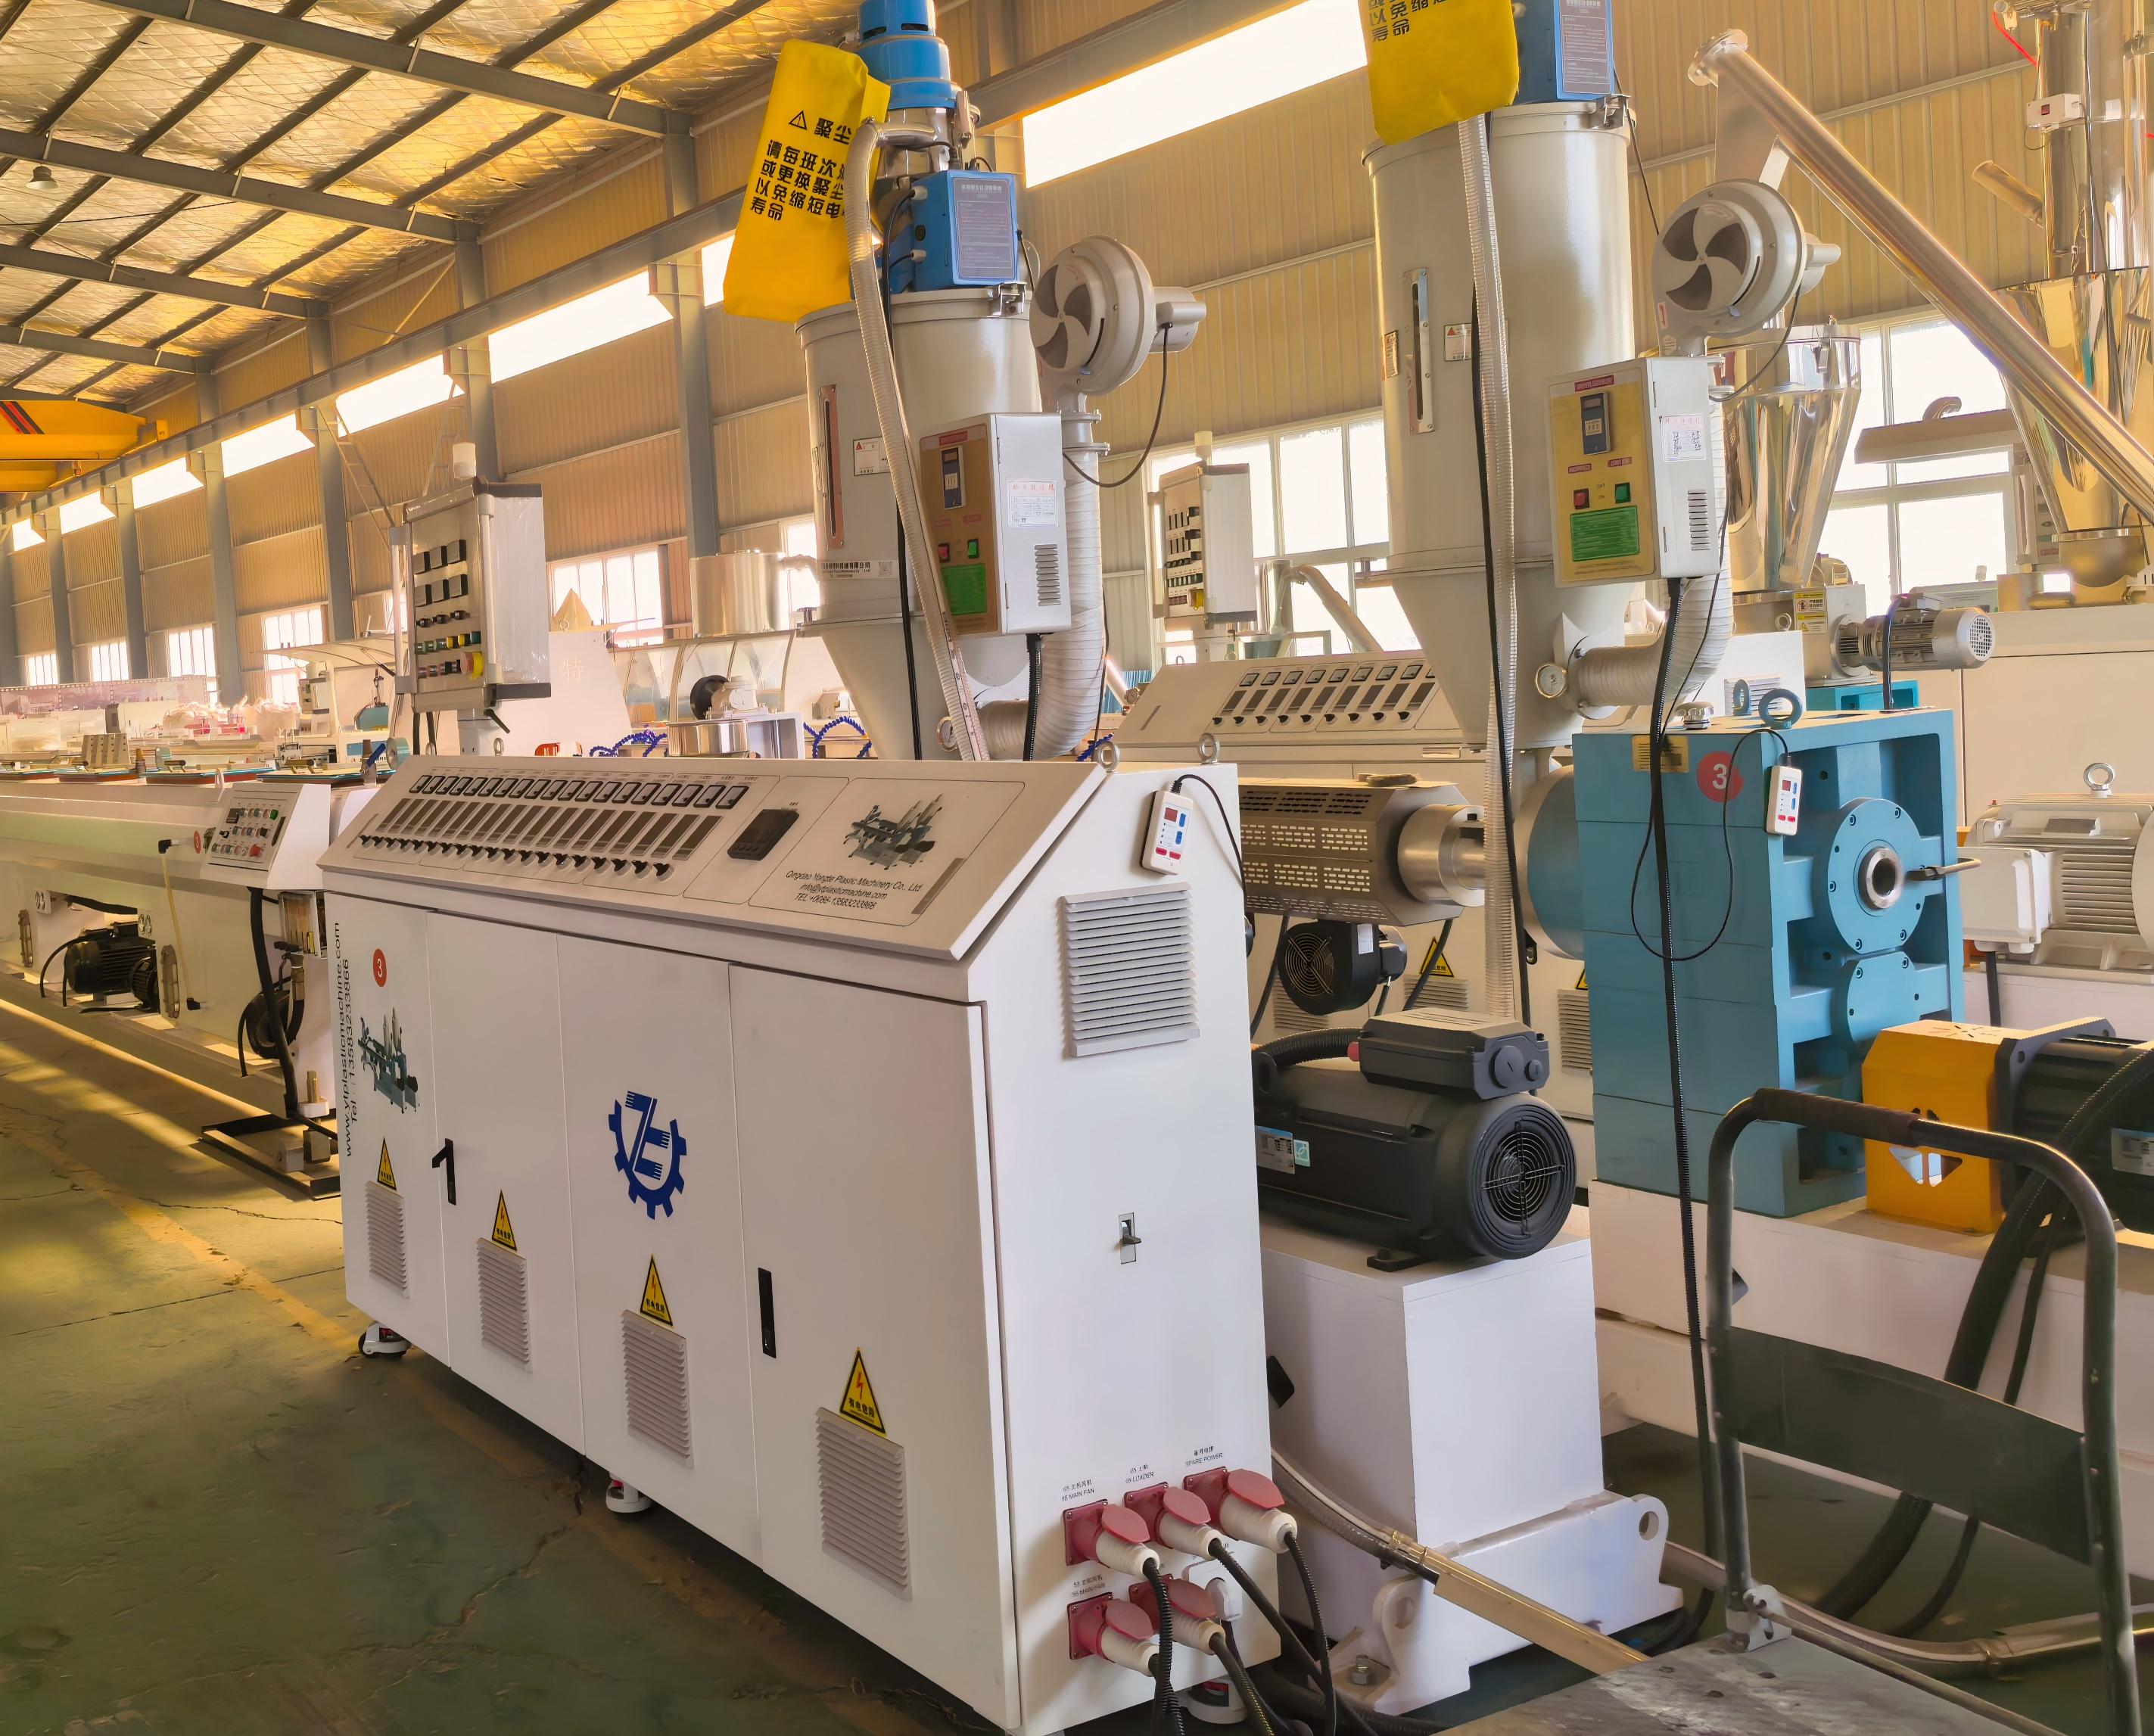
Most PE pipe failures can be traced back to a single overlooked variable on the factory floor. At Yongte, we decided to stop treating that variable as unavoidable. The result is a series of machine-line innovations—from screw geometry to cooling calibration—that consistently produce pipe walls with tighter tolerances and fewer hidden stress points. This isn't a standard equipment catalog pitch. It's a look inside how a PE pipe machine factory rethinks every stage of production when the goal shifts from "acceptable yield" to "predictable high quality." Read on if you're ready to question a few long-standing assumptions.
Precision Extrusion Redefines Wall Consistency
Precision extrusion has quietly upended what manufacturers consider achievable in wall consistency. Rather than accepting the subtle drift in thickness that plagues standard runs, this process locks diameter and wall variance into a range once reserved for machined parts. The result is tubing and profiles that behave predictably under pressure, heat, or repeated flexing — no more guessing where the thin spot hides.
What sets this approach apart isn't a single breakthrough, but a chain of tight controls: real-time laser measurement feeding back into screw speed, die geometry tuned for the specific resin's melt memory, and downstream calibration that corrects ovality before it freezes. That feedback loop catches deviations early enough to adjust mid-run, so the final reel matches the first meter instead of drifting toward the tolerance edge.
For engineers, the payoff shows up in fewer rejected batches and less over-engineering to compensate for weak walls. Catheter shafts hold their ID under torque, multi-lumen tubing keeps each channel's flow rate steady, and thin-wall heat shrink doesn't bunch or tear at the seam. When wall consistency becomes a given rather than a goal, designs stop apologizing for the manufacturing process and start exploiting it.
Smart Heat Zones Adapt to Raw Material Shifts
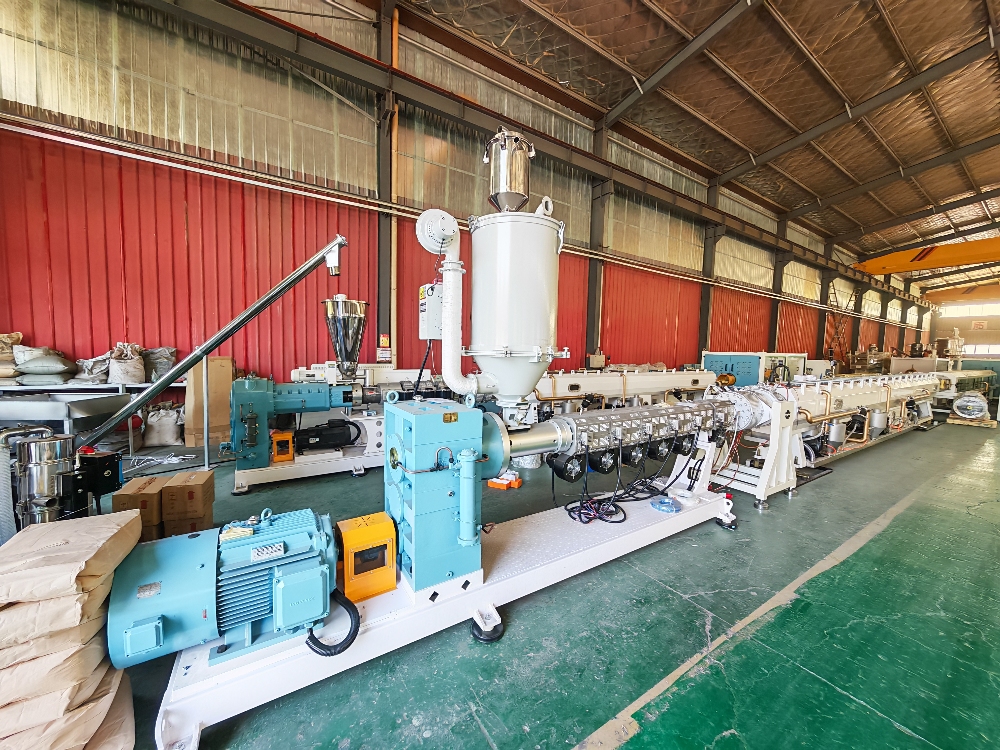
Most heating lines still run on a single, fixed recipe. That works fine until a supplier switches ore sources or a batch of recycled scrap arrives with higher moisture. Smart heat zones take a different approach: each segment of the furnace watches the material entering it and adjusts its output on the fly. A wetter, denser load gets more energy exactly where it's needed, while a lighter or drier section avoids unnecessary heat.
The trick is in the feedback loop. Temperature sensors, moisture probes, and sometimes inline composition analyzers feed data to a control system that constantly remaps the ideal thermal profile. If the raw material's thermal conductivity drops mid-shift, the zones closest to the cold spots ramp up before the rest of the line even notices. Operators see a live heat map instead of guessing from thermocouple averages.
That kind of responsiveness matters most when raw material quality drifts over weeks rather than hours. Plants using smart zoning can hold tighter product tolerances without repeatedly stopping to recalibrate. They also burn less fuel, since energy is never wasted on zones that already have enough heat. In practice, it turns a rigid production line into something closer to a living system.
Quick-Change Heads Keep Lines Running Longer
In most production environments, switching between product formats or replacing worn tooling means shutting down the whole line and losing valuable minutes—sometimes hours—to disassembly and recalibration. Quick-change heads flip that script. They’re built around a modular, pre-aligned design that lets an operator unlock the old head, slide in the new one, and lock it into place without touching a single adjustment screw. What used to take a full maintenance crew half a shift now happens in the time it takes to grab a coffee.
The real payoff shows up in cumulative uptime. Because changeovers become a quick, predictable step, planners can schedule more product variety into a single shift without fearing the downtime penalty. And when something does go wrong mid-run, swapping in a spare head gets the line moving again fast instead of forcing a lengthy teardown. It’s about keeping the bottleneck where it belongs—on actual production speed, not on setup overhead.
On the floor, crews notice the difference immediately. Heads are often keyed or color-coded to prevent mismounting, and the locking mechanism gives a satisfying, foolproof click. Fewer tools left scattered around the work area, fewer rushed adjustments under pressure, and a line that keeps humming through change after change.
Vision Systems Catch Flaws Human Eyes Miss
Machine vision systems operate on wavelengths and frame rates that far exceed human perception. They can detect hairline cracks in turbine blades, micro-delamination in composite panels, or sub-pixel misalignments on circuit boards—all without fatigue or attention drift. Unlike an inspector who might blink at the wrong moment, these cameras capture every frame, and algorithms compare each pixel against a learned baseline, flagging even the faintest anomaly.
The real advantage emerges in high-speed production lines where flaws appear for only a few milliseconds. A human eye simply cannot register a defect moving past at several meters per second, but a line-scan camera paired with strobing illumination freezes that moment, revealing scratches, voids, or color shifts that would otherwise slip through. This extends beyond simple detection—advanced systems learn from historical defect data, adapting to new failure modes without explicit reprogramming.
In practice, this means fewer recalls, less scrap, and higher confidence in safety-critical parts. Automotive suppliers use these systems to inspect weld seams inside chassis cavities where no human could ever look. Electronics manufacturers catch solder bridges thinner than a human hair. The result isn't just automation—it's a fundamental shift in what "good enough" means, because the system never gets bored, never assumes, and never misses what it was trained to see.
Energy-Saving Drives Pay Back Through Lower Bills
Motors account for a large share of industrial electricity use, and running them at full speed when demand is lower wastes a surprising amount of power. A variable speed drive adjusts the motor's output to match the actual load, so a pump or fan that once ran flat-out now slows down during off-peak periods and consumes only the energy it truly needs. This simple change can cut kilowatt-hour usage on a single motor by 20% to 50% in many applications.
Those reductions show up directly on the monthly utility bill. A drive often pays for itself within 6 to 24 months, and after that the lower energy cost becomes recurring savings year after year. In facilities with multiple motors, swapping fixed-speed starters for energy-saving drives can turn a noticeable overhead expense into a predictable, smaller line item.
Bespoke Die Designs Unlock Niche Pipe Profiles
Standard extrusion tooling tends to settle around a familiar set of round, square, or rectangular profiles because those are easy to balance and cool. Bespoke die work breaks that mould by engineering flow channels around asymmetric walls, internal ribs, integrated snap-fit grooves, and co-extruded sealing lips. The real trick is not just shaping the opening, but predicting how the melt will swell, sag, and shrink once it leaves the die, then compensating for those shifts in the steel itself.
Many niche pipe profiles used to require secondary machining, adhesive bonding, or awkward workarounds because no off-the-shelf die could hold the geometry. A custom die collapses those steps into a single extrusion pass, which often improves wall consistency and removes weak joints. For small-batch industrial tubing, medical conduits, or architectural channels, that shift can mean the difference between a part that barely works and one that drops straight into assembly.
The trade-off is that bespoke tooling demands a tighter loop between design, simulation, and trial runs. Flow balancing software gets you close, but it rarely accounts for every resin lot variation or the thermal quirks of a specific extrusion line. Experienced die makers lean on iterative corrections, adjusting land lengths or choke points after the first sample run. That back-and-forth is what separates a proprietary profile from a generic tube, and it is why manufacturers will pay a premium for a die that actually unlocks a shape nobody else can run.
FAQ
Instead of relying on older single-stage cooling, newer lines integrate vacuum calibration sleeves and multi-zone thermal control, which keeps wall thickness uniform even at higher line speeds.
Incoming resin batches are tested for melt flow rate and moisture before blending; real-time gravimetric dosing then adjusts the feed to match the extruder's torque curve, preventing surging and dimensional drift.
Grooved barrels create a positive conveying zone, so output stays stable even with recycled content or lower bulk density regrind, reducing pressure fluctuations that can lead to weld line defects.
Ultrasonic wall thickness gauges and laser diameter sensors scan continuously, feeding data back to the haul-off and screw speed; any deviation beyond 0.2 mm triggers an automatic mark for downstream rejection.
Yes, line builders now fit adaptive barrel heating with ceramic bands and use waste heat from the cooling tanks to pre-dry raw material, cutting overall energy use per meter by up to 15 percent.
With modular co-extrusion blocks and quick-change die heads, the changeover takes under two hours, letting a single line run HDPE solid, PE100-RC, or barrier-layer pipe without major downtime.
Each production batch gets a digital twin record with melt pressure, cooling rate, and haul-off tension; operators can compare historical traces to catch slow drift in screw wear or calibration sleeve fouling before it causes rejects.
Spiral mandrel dies with polished chrome surfaces and optimized land lengths distribute melt evenly, so linear speeds can reach 30 meters per minute while keeping the inner surface smooth and free from sharkskin.
Conclusion
Modern PE pipe machines have moved far beyond simple screw-and-barrel setups. Precision extrusion now actively corrects wall thickness in real time, cutting the once-common drift that led to weak spots or overweight pipe. Smart heat zones read the actual melt behavior of each resin batch and adjust barrel temperatures on the fly, so a shift in raw material supply never turns into burnt specks or poor fusion. Quick-change heads add another layer of uptime, operators swap out die and calibrator sets in minutes instead of hours, and the modular design tolerates frequent size changes without losing alignment. Together these upgrades keep the line running at full speed while dimensional consistency stays tighter than older machines could ever deliver.
Quality control no longer depends on a worker's eye alone. Vision systems scan the pipe surface and weld line at high frame rates, flagging micro-cracks, bubbles, or ovality that human inspectors routinely miss. When a flaw appears, the line can mark the section for rejection before it reaches the coiler, saving downstream waste. Energy-saving drives quietly reduce power draw during low-load cycles, and the monthly electricity savings often cover the upgrade cost within a couple of years. Bespoke die designs have become a factory's secret weapon for niche pipe profiles, whether that means corrugated drainage pipe, multi-layer barrier tubing, or custom diameters for industrial clients. Each innovation reinforces the others, turning a standard PE pipe machine factory into a flexible, high-quality production hub that adapts to changing orders without sacrificing repeatability.
Contact Us
Contact Person: Ms Qin
Email: [email protected]
Tel/WhatsApp: 8613583233866
Website: https://www.yongteplast.com