
China Threaded Reinforcing Bar Socket Selection Guide for Structural Projects
2026-10-23
Selecting the right threaded reinforcing bar socket can make or break a structural project’s integrity and schedule. In China’s fast-paced construction landscape, the choices are vast but not all equal. This guide cuts through the noise, drawing on field-tested criteria to help you match socket specifications to real-world loads, corrosion exposure, and installation constraints. Whether you’re upgrading a high-rise core or anchoring a bridge deck, understanding the subtle trade-offs in thread engagement, steel grade, and coating systems is critical. And when reliability is non-negotiable, brands like Sinou have earned their place on shortlists by consistently delivering dimensional accuracy and ductile failure modes. Read on to discover the key factors that separate a socket that merely fits from one that performs for decades—and why many engineers are rethinking their default specs.
Reading Thread Profiles to Avoid Mismatched Sockets
A quick glance at a threaded fitting rarely tells the whole story. Two connectors might share the same outer diameter and even feel like they start to engage, but a careful reading of the thread profile often reveals differences in flank angle, pitch, or taper that would lead to a poor seal or stripped threads. This is why experienced technicians treat the profile itself as a primary identifier rather than relying on nominal size alone.
Reading a thread profile means examining the cross-sectional shape of the groove and crest. Using a thread gauge or an optical comparator, you can measure the angle between flanks, the depth of the cut, and the spacing from one crest to the next. For example, a 60-degree included angle is common in metric and UN threads, while many pipe threads use a 55-degree angle. Spotting that single difference can stop you from forcing a BSP fitting into an NPT port.
In practice, mismatches often happen when parts are cleaned and mixed in the same bin or when a replacement is ordered from memory. Taking a few seconds to read the profile against a known reference saves more than time; it prevents damage to expensive components and avoids leaks that only show up under pressure. The habit becomes second nature once you have seen how easily a near-match can turn into a cross-threaded failure.
What Chinese Mill Certificates Actually Tell You
A Chinese mill certificate is rarely a straightforward guarantee of material quality — it's more like a snapshot of what the mill claims happened in a specific heat or batch. The first thing to understand is that the values listed for chemical composition and mechanical properties are often not the average of the entire production run, but the results from a single test specimen taken under ideal conditions. Whether that specimen truly represents the steel you receive depends heavily on the mill's internal sampling discipline, and that discipline varies more between Chinese producers than most buyers expect.
You'll also notice that many certificates from smaller or mid-sized mills include only the mandatory elements required by the relevant standard, while leaving out trace elements that could affect weldability or corrosion resistance. A certificate that lists, say, carbon, manganese, silicon, sulfur, and phosphorus — but omits chromium, nickel, copper, or nitrogen — isn't necessarily hiding anything, but it also doesn't tell you whether the material will behave as expected in a demanding application. The real value comes from comparing the certificate's stated heat number to the physical marking on the product and checking whether the mill actually performed the tests it claims, or simply filled in nominal values from a previous batch.
Finally, what a Chinese mill certificate tells you is only as good as the mill's internal traceability system and its willingness to stand behind the document. Top-tier mills now issue certificates with QR codes linking to digital records, which reduces the risk of forged or duplicated documents. But even with those systems, you should treat the certificate as a starting point for verification rather than a final answer. Independent retesting of critical shipments — especially for structural steel or pressure vessel components — remains the most reliable way to find out whether the certificate's numbers match the steel in your hands.
Choosing Yield Strength Overmatch for Site Conditions
Field conditions rarely match the idealized assumptions in welding codes. A pipeline laid across permafrost behaves differently than the same joint tested in a climate-controlled lab. When a weld is specified with yield strength overmatch, the intent is to keep plastic strain localized in the base metal rather than the filler. But on site, low ambient temperature can reduce the fracture toughness of that higher-strength weld metal, turning a conservative design into a crack initiation point. So the first step is not to blindly accept a standard overmatch percentage, but to ask what the ground, weather, and loading history will actually impose on that joint.
High restraint is another field reality that gets overlooked. Thick-wall tie-ins, repair welds in awkward positions, or joints made with the pipe still under residual stress from laying—these conditions multiply the local stress concentration. An overmatched weld in a highly restrained joint may never yield as intended, instead driving the failure to the heat-affected zone or even into the weld itself. Some contractors push for even higher overmatch to compensate, but that often backfires by increasing hardness and hydrogen cracking susceptibility. The better approach is to map the actual restraint level with strain gauges or finite element models before choosing the filler metal.
Practical selection comes down to a few simple checks. For arctic or subsea work, lower the overmatch target by 5-10% and specify a filler with guaranteed Charpy values at the lowest service temperature—not the design minimum, but the coldest night the line is likely to see. For sites with seismic activity or known ground movement, a moderate overmatch of 10-15% combined with high elongation in the weld metal often outperforms a very high overmatch that sacrifices ductility. And always keep a record of actual field weld test results. Two different sites can have the same code requirement but completely different answers once you account for real restraint, temperature swing, and installation sequence.
Torque and Assembly Checks Before Concrete Placement
A reliable pour starts well before the first truck arrives. On our last elevated deck, we found two formwork brackets that had loosened during rebar tying—something a visual check alone would have missed. Running a calibrated torque wrench over every anchor bolt, tie rod, and clamp takes time, but it catches exactly that kind of drift. We work through a marked sequence, usually from the center outward, and record the readings instead of trusting memory.
Assembly checks are just as much about geometry as hardware. A quick string line across the top of the bulkhead can reveal a 6 mm sag that would otherwise become a visible step in the finished slab. We also verify that any embedded plates, sleeves, or blockouts are still locked in place after the crew has walked the formwork. If something has shifted, fixing it now is a ten-minute job; after the concrete sets, it's a core drill and an unhappy client.
The torque and assembly log gets signed before the pump line is connected. This isn't paperwork for its own sake—it forces the crew to slow down and look at the connections that will carry several tons of wet concrete. A single overlooked wedge or a bolt at half its specified torque can turn a routine placement into a blowout. When the log is clean, the pour usually is too.
Corrosion Protection: Coatings, Epoxy, or Weathering Steel
When steel structures face aggressive environments, engineers weigh three core options: barrier coatings, epoxy systems, and weathering steel. Barrier coatings—such as high-build polyurethanes or zinc-rich primers—physically isolate the metal from moisture and oxygen, but they demand meticulous surface prep and periodic recoating. Epoxy stands out for industrial settings: its dense cross-linked film resists chemical attack and abrasion, often serving as the middle layer in a multi-coat system. Yet epoxies can chalk under UV unless top-coated, which adds labor and cost.
Weathering steel takes a different path. By alloying copper, chromium, and nickel, it forms a stable patina that actually shields the base metal—no paint needed. This works brilliantly in alternating wet-dry cycles with moderate pollution, but fails in continuously damp, marine-salt, or deicing-salt exposure where the patina can't stabilize. Bridges and transmission towers often favor this approach for its lower lifetime maintenance, though designers must detail joints to avoid crevice corrosion and account for early runoff staining on adjacent surfaces.
The right choice hinges on exposure severity, access for future maintenance, and aesthetics. A coastal chemical plant might specify a three-coat epoxy system with a UV-resistant polyurethane topcoat, while a rural highway overpass could use bare weathering steel from day one. Coating thickness, edge retention, and holiday testing separate durable jobs from premature failures—performance lies less in the product name than in the application rigor and environmental match.
Reconciling Project Specifications with Chinese Standards
Adapting international project specifications to align with Chinese standards often reveals subtle mismatches that go beyond simple unit conversions or material substitutions. The real work begins when design assumptions rooted in Eurocodes or ASTM practices meet the prescriptive language of GB codes. For instance, a structural tolerance considered acceptable under one framework may fall outside the mandatory range in another, forcing engineers to re-evaluate connection details and load paths rather than merely swapping reference numbers. This reconciliation is less about translation and more about translating intent—understanding why a standard demands a particular safety factor and finding a locally compliant way to preserve that intent without compromising the original performance criteria.
A practical approach involves mapping each critical specification item to its nearest Chinese equivalent early in the project, while flagging areas where no direct counterpart exists. During a recent industrial facility upgrade, the discrepancy between fire resistance ratings for cable trays was resolved not by accepting the lower domestic baseline, but by proposing a layered protection scheme that exceeded both the foreign specification and the local code. Such solutions emerge when teams treat Chinese standards not as constraints to be negotiated but as a baseline to be strategically enhanced. This mindset shifts the conversation from compliance anxiety to engineering judgment, where the goal is a coherent system that satisfies both the letter of local law and the performance expectations of the original design.
Documentation becomes crucial because reviewers will scrutinize the logic behind every deviation. Instead of presenting a simple compliance matrix, successful projects embed the reconciliation narrative into the design dossier—explaining, for example, why a Chinese seismic detailing provision was adopted wholesale while a welding procedure was modified to meet both GB and ASME requirements through a single qualified process. This proactive transparency reduces approval cycles and builds trust with local authorities, who are often more receptive to technically justified adaptations than to blanket claims of equivalency. Over time, the reconciliation process itself becomes a knowledge asset, informing future bids and preventing costly redesign loops late in construction.
FAQ
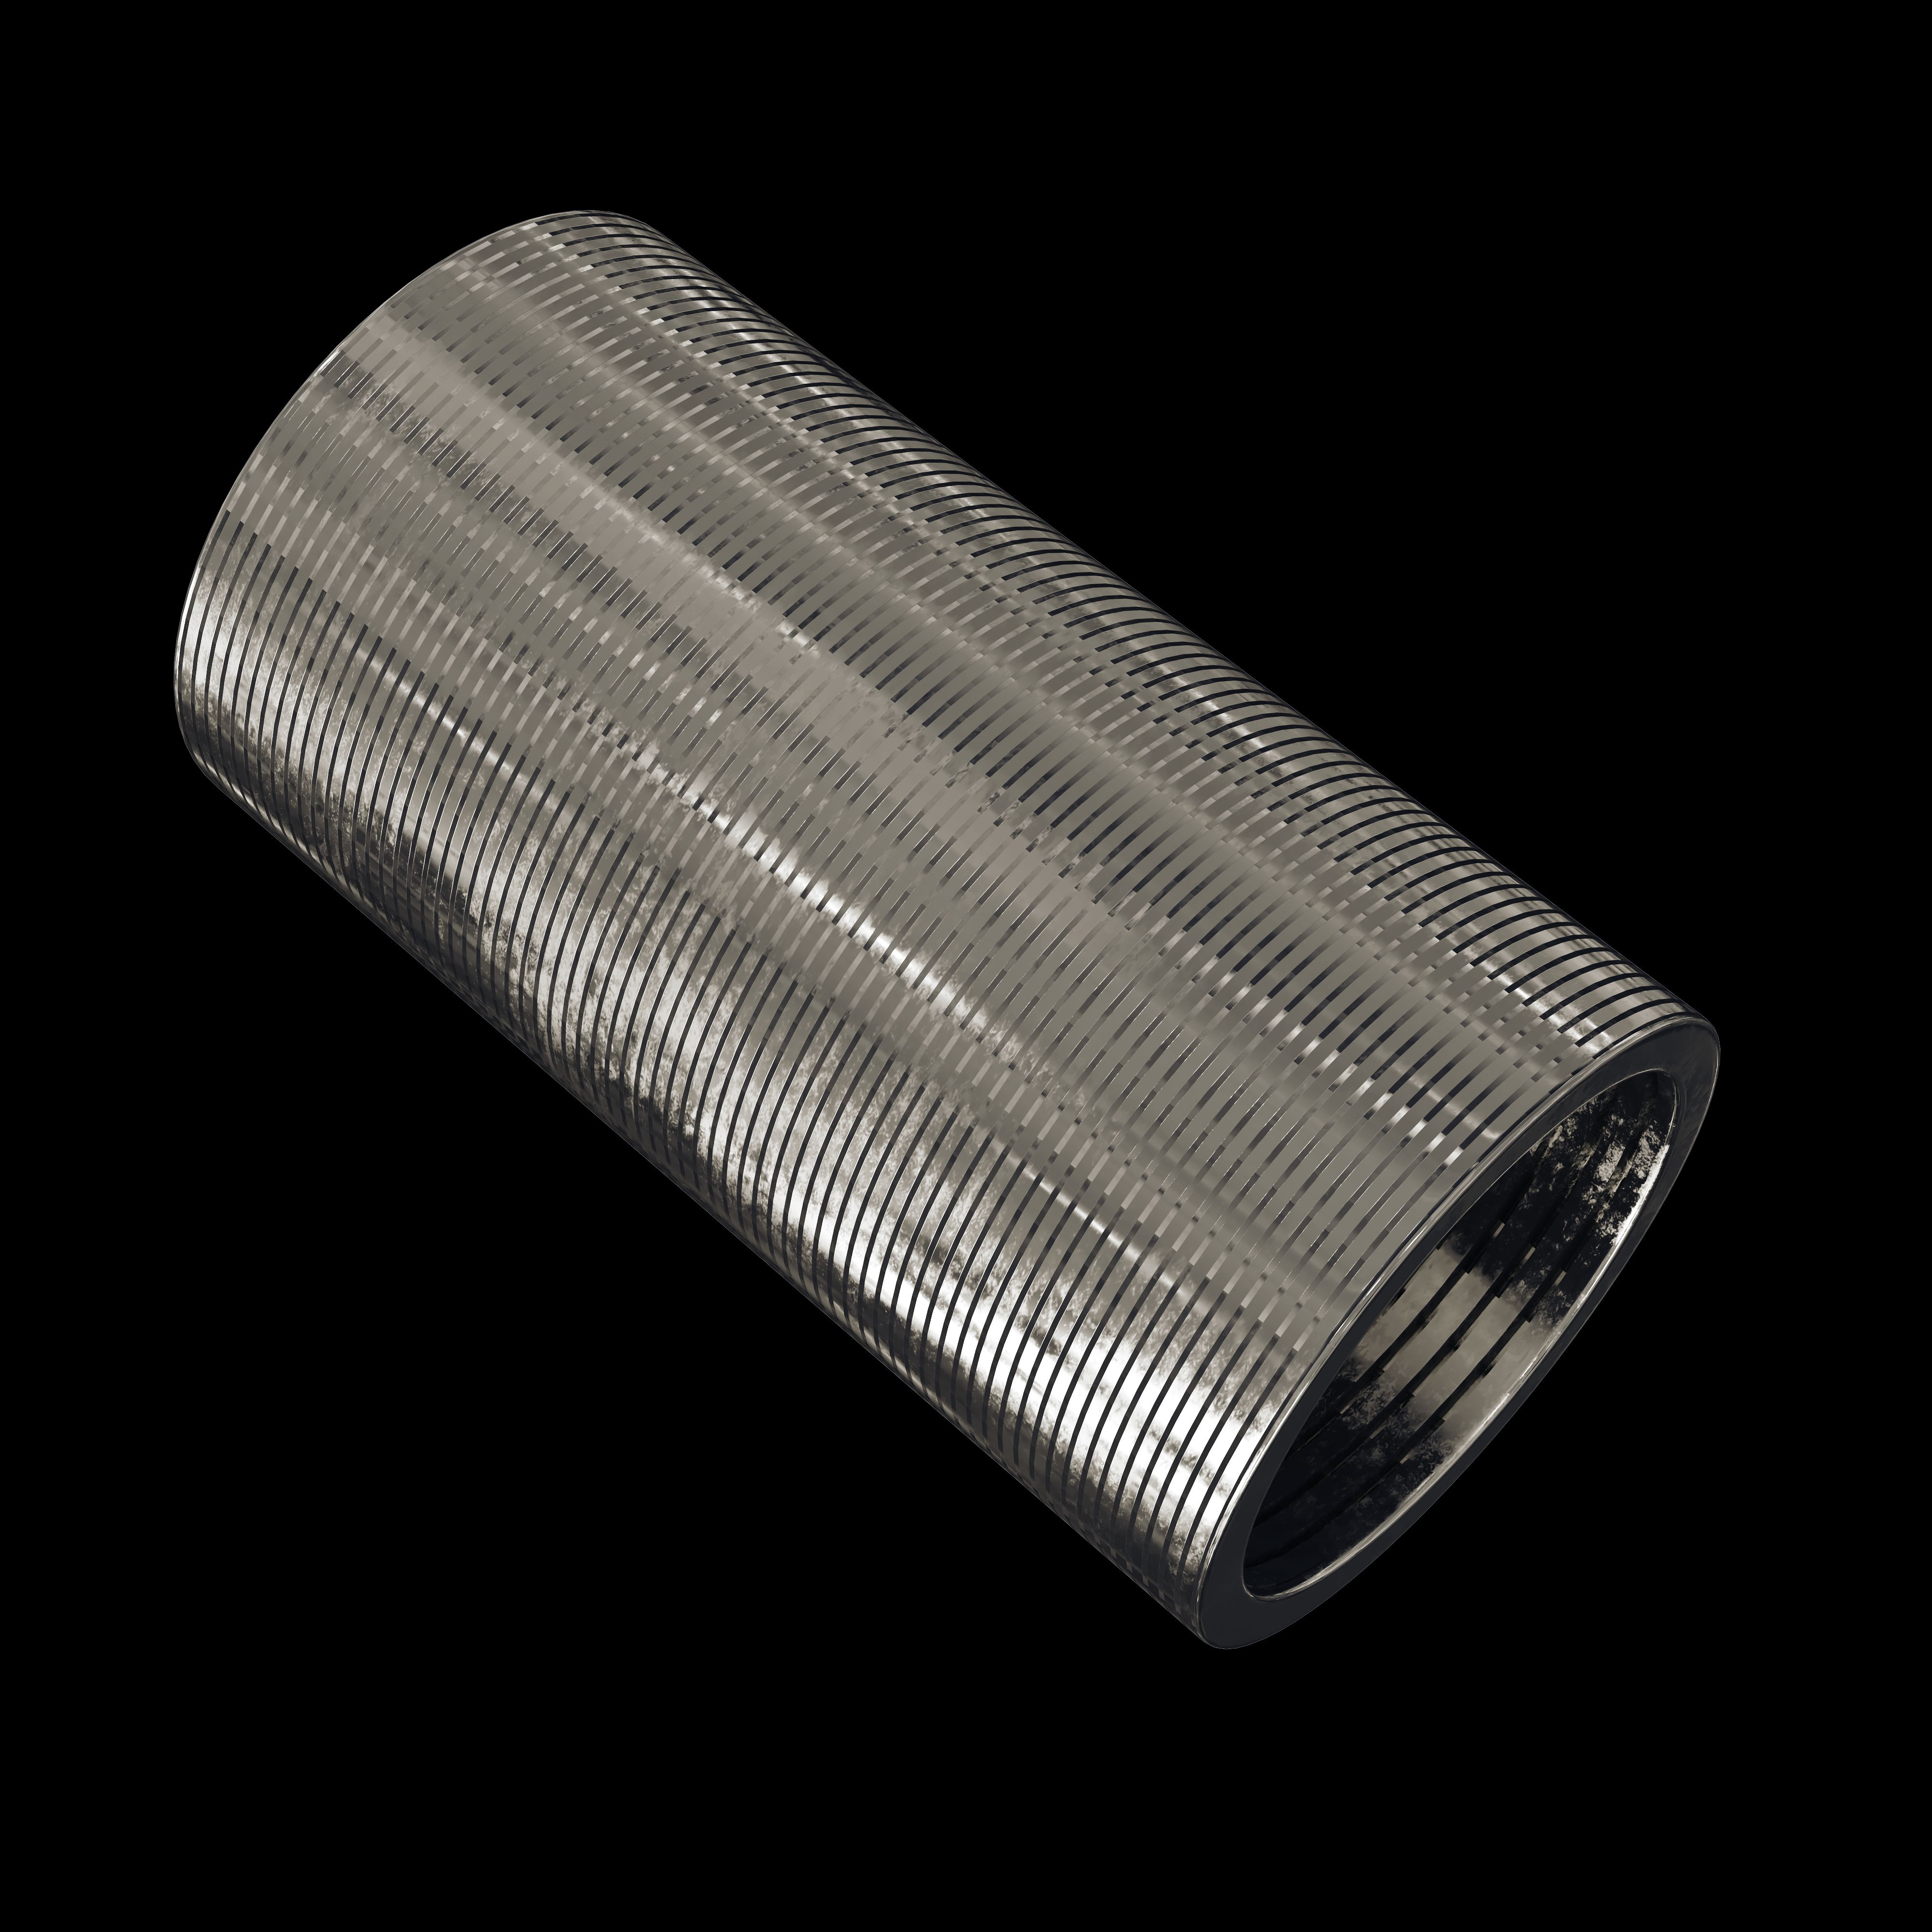
In China, the common types include parallel threaded couplers, tapered threaded couplers, and grout-filled sleeve couplers. Parallel threaded couplers are widely used for standard rebar connections due to their simplicity and reliability. Tapered threaded couplers offer self-aligning properties and are preferred for larger diameter bars or when bar ends may have slight irregularities. Grout-filled sleeves are typically reserved for precast concrete connections where bars cannot be rotated during installation.
The primary standard is JGJ 107, Technical specification for mechanical splicing of steel reinforcing bars. It defines performance grades (Grade I, II, III) and testing requirements. Additionally, JG/T 163 covers the couplers themselves, specifying dimensions, materials, and manufacturing tolerances. GB 1499.2 sets requirements for the reinforcing bars, ensuring the threads are compatible with coupler specifications.
Grade I couplers are designed to develop the full tensile strength of the connected bars and are required for connections in high-seismic zones or critical structural members. Grade II couplers develop at least 100% of the yield strength but less than the ultimate tensile strength, suitable for moderate demands. Grade III couplers are used for non-structural or lightly loaded applications where only basic mechanical interlock is needed. Your choice should follow the project's seismic design category and structural engineer's specifications.
Chinese threaded couplers typically cover rebar diameters from 12 mm to 50 mm. The most common sizes in structural projects are 16 mm through 32 mm. For bars above 40 mm, you may need custom-machined couplers or special thread profiles because standard rolling equipment has limitations. Always confirm the coupler's diameter range matches the design bar size and allows for thread depth that does not reduce the bar's cross-sectional area below code limits.
Yes. In seismic zones, connections must meet stricter cyclic loading requirements. JGJ 107 requires that Grade I couplers pass low-cycle fatigue tests with repeated tension and compression cycles. Avoid using couplers that have not been tested for cyclic performance. Also, stagger splice locations so no more than 50% of bars are spliced at the same cross-section, and ensure couplers are not placed within plastic hinge regions unless explicitly approved.
For normal indoor environments, plain carbon steel couplers with light oil coating are acceptable. In coastal or aggressive environments, specify hot-dip galvanized or epoxy-coated couplers. The coating thickness should be at least 70 µm for galvanizing and 200-300 µm for epoxy. Ensure the coating does not affect thread engagement—overly thick coatings can prevent proper tightening. For concrete with chloride exposure, consider using stainless steel couplers or adding a protective sleeve over the connection.
Installers must use calibrated torque wrenches to tighten couplers to the manufacturer's specified torque. Visual inspection checks that no thread is exposed beyond the coupler and that the bar ends are fully seated. Non-destructive testing methods like ultrasonic or radiographic testing can be used for critical connections. Destructive pull-out tests on sample splices are mandatory according to JGJ 107, typically one test per 500 joints or as specified by the project QA plan.
Yes, but the coupler's internal threading must be designed to accommodate the coating thickness. If the bar is coated before threading, the threads should be re-cut or cleaned to ensure proper engagement. Alternatively, use couplers with larger thread tolerances or specify that bars be threaded before coating and then protected with a cap during coating. Always verify compatibility with the coupler manufacturer, as some coatings may crack under thread rolling stresses.
Conclusion
Selecting the right threaded reinforcing bar socket for Chinese structural projects demands more than matching diameters. A close reading of thread profiles is essential—Chinese rebars often use specific thread forms and pitches that differ subtly from other regional products, and an apparently compatible socket can bind or loosen under load if thread geometry is overlooked. Mill certificates from Chinese suppliers provide useful data, but they require interpretation: look beyond the stated grade to confirm actual chemical composition, elongation, and tensile test results, since variations among mills can affect socket performance. In many cases, specifying a socket with a yield strength slightly higher than the rebar—often called strength overmatch—proves beneficial on sites where bending, splicing, or seismic detailing imposes extra demands. This overmatch helps prevent local yielding inside the coupler before the bar reaches its design capacity.
Before concrete placement, torque and assembly checks should be routine. A socket that is not fully engaged or torqued to the manufacturer's specified value can exhibit excessive slip or premature failure, so a calibrated wrench and visual verification of thread engagement depth are practical safeguards. Corrosion protection deserves equal attention: hot-dip galvanizing, fusion-bonded epoxy, or using weathering steel sockets may be appropriate depending on exposure, but compatibility with the rebar coating must be confirmed to avoid galvanic or bond issues. Finally, reconciling project specifications with Chinese standards—such as GB/T or JGJ series—requires careful side-by-side review, because Chinese standards often use different notation, testing methods, and acceptance criteria. Rather than forcing a direct substitution, engineers should map performance requirements to the relevant clauses and document any deviations clearly. This approach reduces mismatches on site and keeps the structural connection robust through its service life.
Contact Us
Contact Person: HaiYan
Email: [email protected]
Tel/WhatsApp: +86 18957325588
Website: https://www.senyoubeton.com/