
Best Tumble Shot Blasting Machine Factory: Your Ultimate Guide to Quality and Innovation
2026-10-02
When it comes to surface preparation, the right tumble shot blasting machine can mean the difference between a flawless finish and costly rework. Yet with so many factories claiming top-tier quality, how do you identify true innovation? PuHua has built a name by pairing rigorous engineering with practical, forward-thinking solutions for manufacturers across industries. In this guide, we’ll cut through the noise and show you what really drives performance, durability, and value in tumble shot blasting—so you can make a confident choice for your production line.
What Actually Separates a Reliable Tumble Blasting Partner from the Rest
Most shops can run a machine, but few understand what the process is doing to your parts. A dependable partner doesn't just hit cycle start and walk away—they watch how the media breaks down over time, adjust blast angles when wear patterns shift, and flag when a particular batch of castings has harder scale than usual. That kind of attention comes from years of troubleshooting, not a laminated checklist. If your current vendor can't tell you the last time they checked the separator or why your finish suddenly turned matte, they're not really managing the process; they're just renting you machine time.
Another tell is how they handle the unglamorous side: dust collection, abrasive replenishment, and preventive maintenance. The reliable ones have a rhythm. You'll notice their hoppers aren't half-empty, their dust legs aren't caked, and they schedule downtime before a breakdown forces it. They also ask about your end use—painting, e-coat, powder, or bare metal—because they know a profile that's too deep or too shallow creates adhesion problems downstream. That conversation rarely happens with a partner who's just pushing parts through to invoice you.
Finally, look at their communication when something goes wrong. A trustworthy blaster will call you the same day they see a quality drift, not ship the lot and hope you don't notice. They'll bring data—media consumption rates, blast pressure logs, wheel amp readings—and a proposed fix. That level of transparency is rare, and it's exactly what separates a vendor who keeps you guessing from a partner who keeps your line running.
Materials and Methods Inside the Build That Define Long-Term Performance
Every structure that stands the test of time does so not by chance, but because of deliberate choices made in materials and construction techniques. The foundation of long-term performance lies in selecting substrates that resist environmental stressors—whether that means high-density concrete with low permeability, fiber-reinforced polymers that shrug off corrosion, or thermally stable alloys that maintain integrity under cyclic loading. It is less about chasing the newest option and more about matching the material's inherent behavior to the specific demands of the site and the expected lifespan. A builder who understands this avoids the trap of over-specifying, which can be just as damaging as cutting corners.
Beyond raw material selection, the methods used to assemble and protect these components determine how well they age. Joint detailing, curing protocols, and protective coatings are not afterthoughts; they are the difference between a system that performs for a decade and one that endures for a century. For example, proper moisture management during the first few weeks of concrete curing can reduce micro-cracking that later accelerates freeze-thaw damage. Similarly, applying a sacrificial anode or a high-build epoxy barrier in the right sequence extends the life of steel elements far beyond what the base alloy alone could achieve. These practices demand field discipline and a respect for dwell times—things that are easy to overlook in a rushed schedule.
What sets truly long-lasting builds apart is the integration of inspection and adaptation into the construction process itself. Rather than treating quality control as a final checklist, leading teams embed material verification and method audits at each phase. Small-batch sampling, non-destructive testing on critical connections, and documenting environmental exposure during construction all feed into a feedback loop. This approach allows for real-time adjustments—like altering a mix design when humidity spikes or delaying a coating application when substrate temperature falls outside the ideal range. It is this combination of informed material choice, uncompromising method execution, and adaptive oversight that quietly defines whether a build will be a legacy or a liability.
Smarter Ways to Finish Surfaces Where Innovation Meets the Shop Floor
Surface finishing has long been the step where good parts go to get ruined—or, occasionally, rescued. A shop can nail every machining tolerance only to lose hours hand-polishing a radius or reworking a chrome layer. The smarter approaches now showing up on real shop floors don't start with fancier abrasives; they start with measuring what actually happens at the contact patch. Handheld profilometers tied to mobile apps, inline laser scanners that flag a 0.2 µm drift before it becomes scrap, and simple torque signatures from rotary tools are giving machinists a feedback loop they never had.
Once that feedback exists, the process stops being guesswork. Shops are pairing adaptive robots with force sensors so a buffing wheel backs off automatically when it crosses a weld seam or a sharp edge. Electrochemical deburring is moving out of aerospace-only territory because small, self-contained cells now fit next to a CNC mill. And laser texturing, once a lab curiosity, can put a consistent grip pattern on a mold or a medical implant without masking or chemical disposal. The common thread is that these tools work with the operator's judgment, not against it.
The real payoff shows up in the numbers nobody romanticizes: abrasive consumption drops, cycle times shrink, and surface roughness stops bouncing between shifts. A toolroom that used to keep three "finish guys" busy for a day now sends one person to monitor a cell that does the same work in two hours. That's not automation for its own sake—it's giving the shop floor a way to predict a finish before a part ever touches the wheel. When innovation lands there, it looks less like a glossy brochure and more like a quieter, cleaner, more predictable shop.
Tailored Blasting Solutions for Unusual Workpieces and Tight Deadlines
Odd-shaped parts rarely fit standard blasting setups. A crankshaft with deep oil channels, a weldment with tight internal corners, or a thin-walled housing all trap abrasive and hide surface defects. Our approach starts with mapping the shadow zones and building custom nozzle angles, masking strategies, and sometimes low-pressure media blends so the blast reaches where it needs to without warping or embedding grit.
Short lead times usually force a choice between speed and finish quality. We avoid that tradeoff by keeping a range of blast media and portable rigs ready, and by running small-batch trials on scrap or off-cut sections of the same material. This gives us a realistic profile reading and cleanliness level before the production run, so the first finished piece is acceptable instead of being a test coupon.
When a deadline is tight and the workpiece geometry is unusual, the real problem is communication. We pair each job with a single point of contact who can read the drawing, adjust the process mid-run, and sign off on surface profile, coverage, and edge retention. It keeps rework off the critical path and gets parts out the door without last-minute surprises.
Questions Worth Asking Before You Visit Any Production Facility
When you tour a production facility, most hosts will lead you past the cleanest lines, the newest equipment, and a few carefully staged workstations. Before you go, write down questions that cut through the staging. Ask to see the defect tracking board for the last six weeks, not the annual summary. Ask how many unplanned line stoppages occurred last month and what the root cause was. Ask to walk through the rework or quarantine area—not just glance at it. If a guide hesitates or says that area is 'not part of the tour,' you've learned something no brochure can teach.
Dig into the people side as well as the machines. What is the average tenure of a line supervisor, and how many operators have been cross-trained on more than two stations? A facility where the same supervisor has run the shift for years and where cross-training records are current is far more likely to catch small problems before they become big ones. Ask to see the last three maintenance logs for the oldest piece of equipment still in daily use; if they can find them in under a minute, that's a sign of a disciplined operation.
Finally, ask about the moments they would rather not discuss: the last safety near-miss, the last supplier failure, the last time a customer rejected a batch. How quickly did they notify affected buyers? What changed afterward? Facilities that can tell you a specific story about a failure and the correction—without blaming someone else—are the ones you can trust when your order is on the line.
Support, Spare Parts, and Continuous Improvement Beyond the Sale
After the equipment leaves the dock, the relationship doesn't end. A support engineer familiar with each serial number is often the first point of contact when a line halts, and that familiarity shortens the time between a midnight phone call and a clear diagnosis. The same engineer can usually tell whether the fix is a simple recalibration or a part that should have been retired two hundred cycles ago.
Spare parts don't sit in anonymous bins. Critical components are staged in regional hubs based on the actual failure rates we've logged from similar installations, not a blanket list. When an unusual part is needed, it gets pulled from teardown stock or, in a few cases, machined overnight and shipped with a tracking link that shows the courier's route in real time.
Continuous improvement is documented as a living log rather than an annual service review. Every intervention triggers a short note in the machine's history: what was replaced, what the wear pattern suggested, and whether a material change or a firmware tweak would make the next 10,000 hours less eventful. Those notes feed small engineering changes that roll out as retrofit kits, sometimes without a formal service bulletin, simply because the data pointed there.
FAQ
Look beyond polished brochures. A trustworthy factory will openly share their frame stress-relieving process, liner material specs, and blast wheel bearing loads. If they hesitate on those details, walk away.
It matters when it cuts cycle time without over-peening delicate parts. Modern machines use variable frequency drives, quick-swap blade wheels, and real-time amperage monitoring to adjust media flow mid-cycle. That kind of control wasn't common ten years ago.
Steel shot and grit remain workhorses for heavy descaling, but ceramic and stainless cut wire are gaining ground for non-ferrous parts. The key is matching abrasive hardness to the component's hardness—too aggressive and you'll embed particles.
Yes, and the best ones will ask for sample parts upfront. They'll adjust barrel speed, door opening, and even the blast pattern to prevent thin-walled components from denting while still cleaning thick castings in the same batch.
Daily checks of the separator screen and dust collector pressure drop are non-negotiable. Also, replacing worn wheel blades on a schedule—not just when they shatter—prevents unbalanced rotation that trashes bearings.
Not necessarily. A mid-priced machine with a Mn13 liner and a direct-drive wheel can outperform a pricier model with inferior wear plates. Focus on total cost per ton blasted, not the sticker price.
Request a video walkthrough of their assembly area, then ask for a third-party test report on a recent machine's blast uniformity. If they can't produce both, their quality claims are likely marketing fluff.
A poorly designed dust collector lets fine particles recirculate, which contaminates the media and dulls the finish. A good system maintains negative pressure inside the cabinet, pulling out fines continuously—otherwise you're just sandblasting with mud.
Conclusion
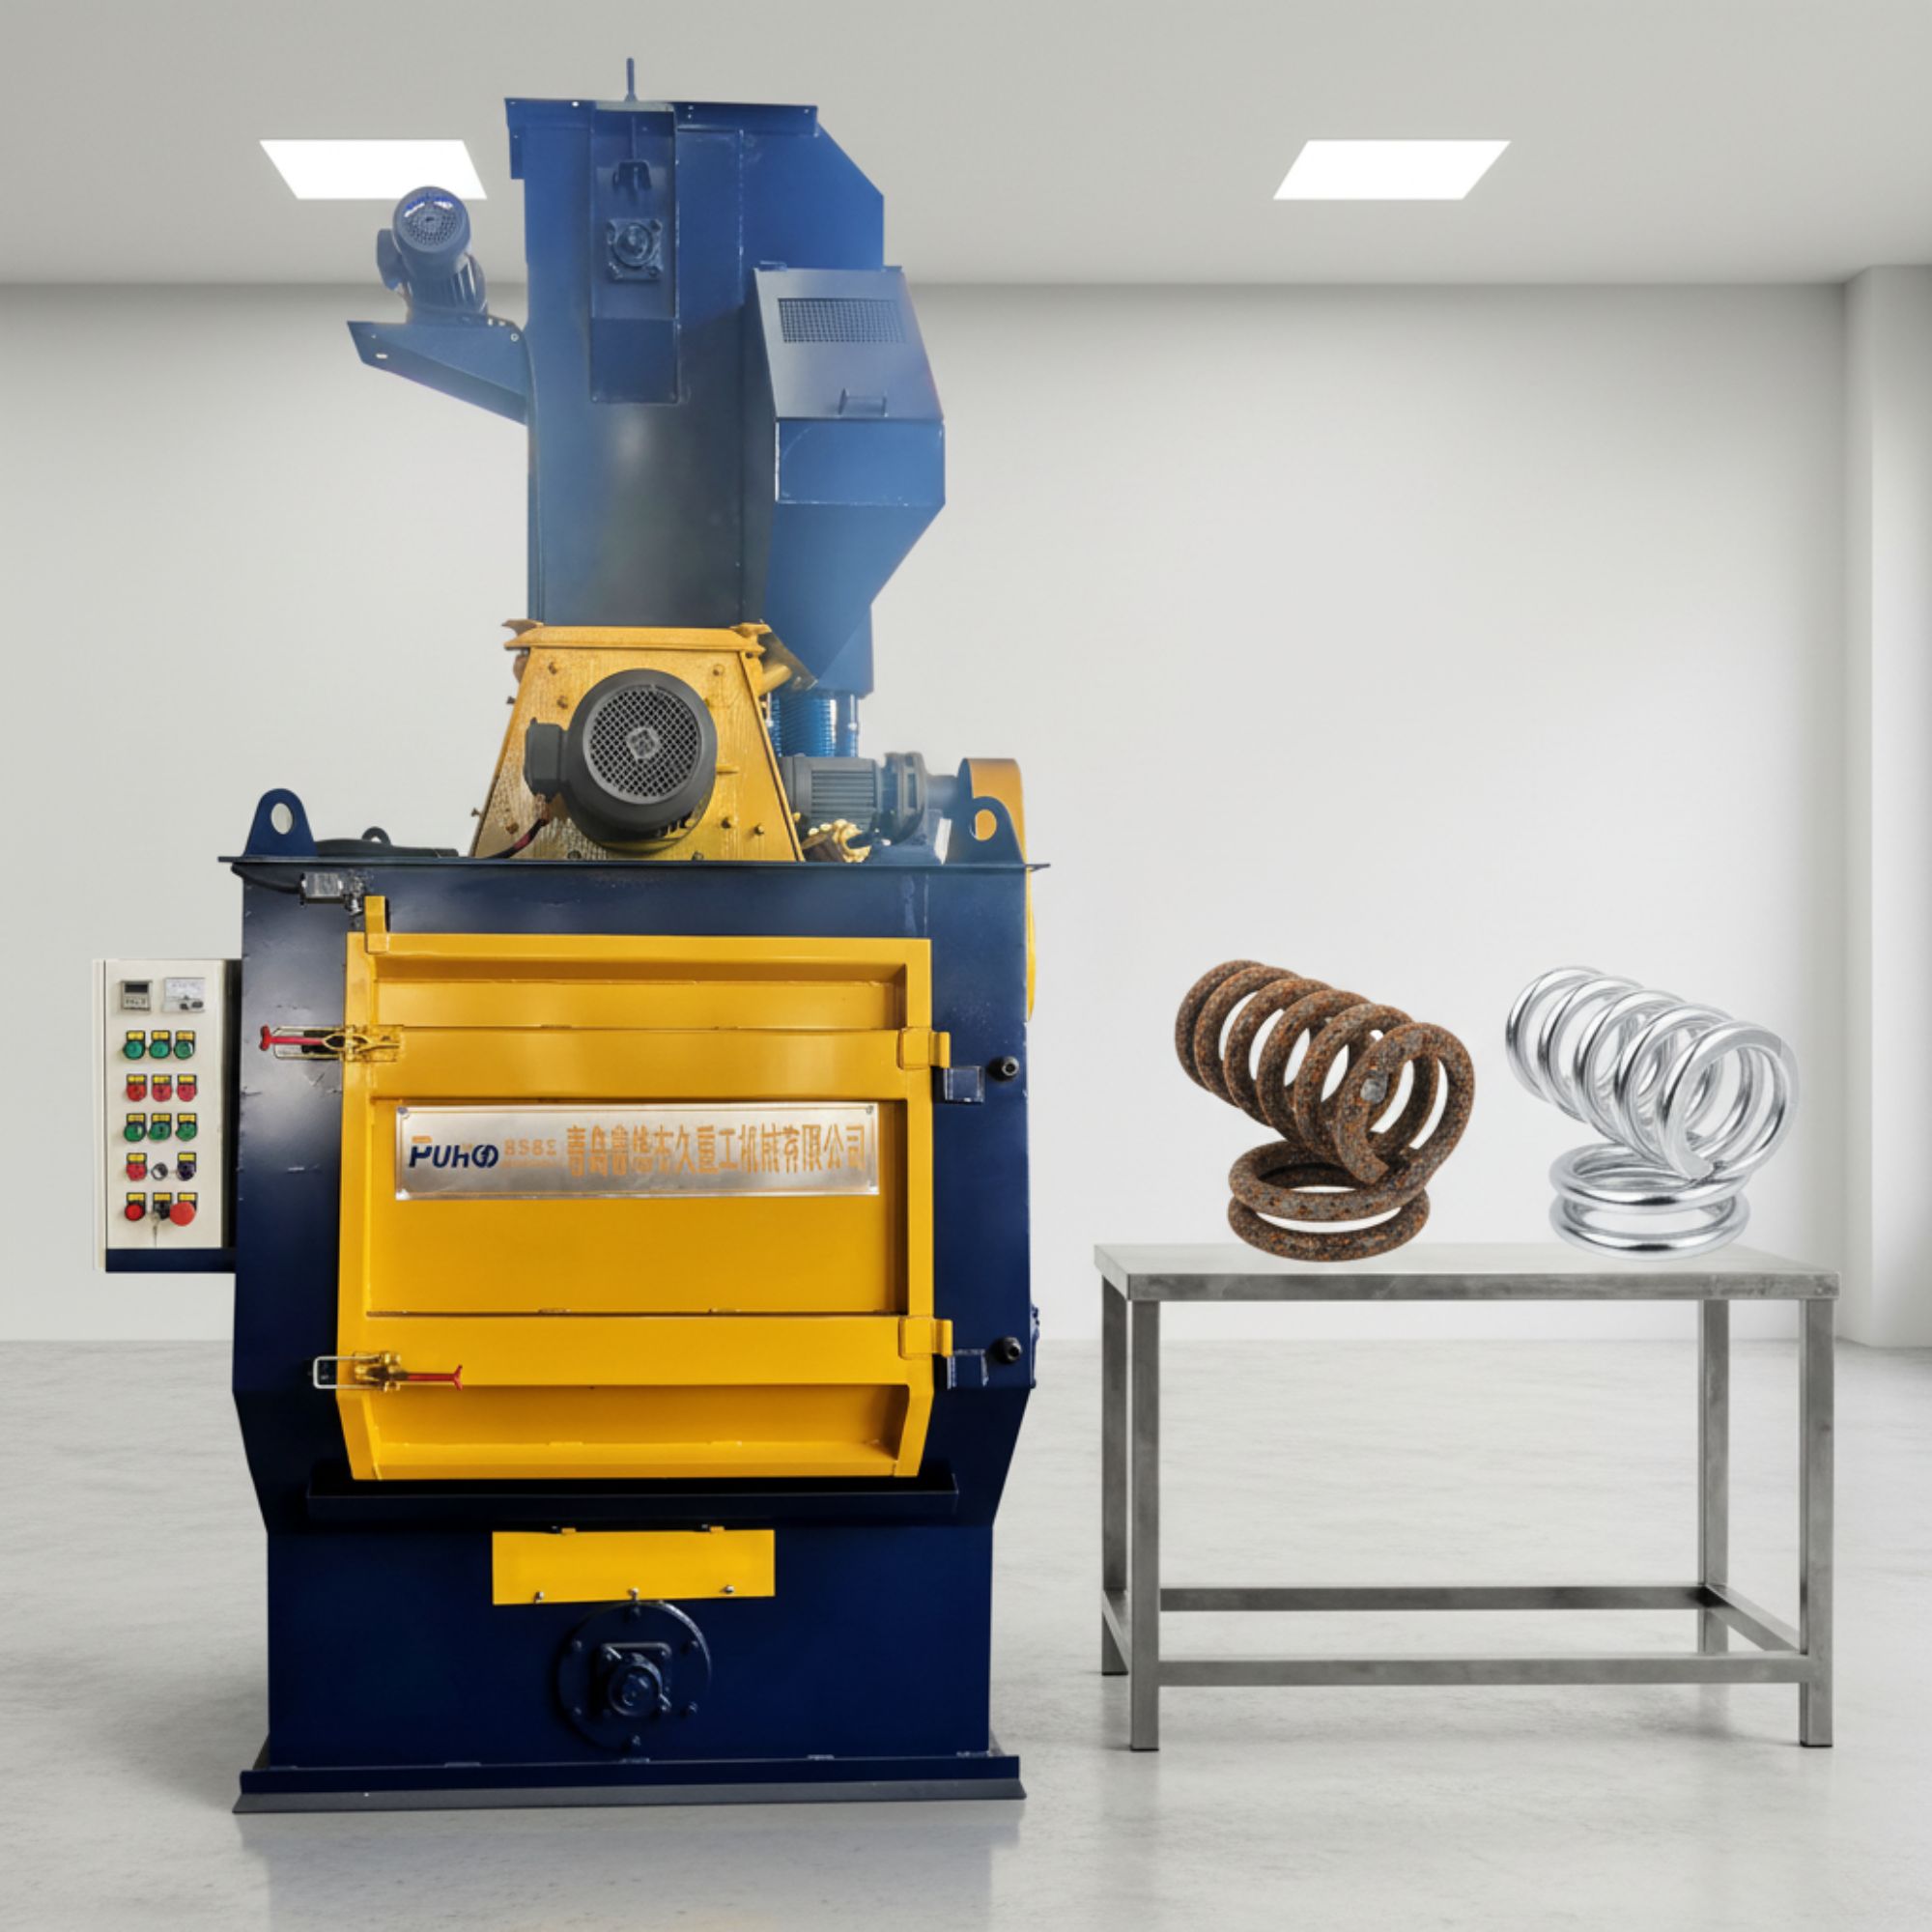
A dependable tumble shot blasting partner stands out not because of polished brochures but through the choices hidden inside the machine. The difference shows up in liner alloys, blast wheel geometry, and the design of the abrasive reclaim system. These details decide whether a machine still holds its pattern and pressure after thousands of cycles. The best factories use high-chrome wear plates, adjustable blast angles, and well-sealed separation chambers, so media flow stays even and hot spots disappear. Long-term performance comes from deliberate welding, bearing selection, and honest material testing, not from a fresh coat of paint. When a builder opens up its parts list and explains why a particular alloy was chosen, that transparency separates a real manufacturing partner from a reseller.
Innovation on the shop floor often means less manual fiddling, more repeatable outcomes. Forward-thinking factories now fit variable-frequency drives, automatic media top-up, and programmable nozzle travel into standard tumble blast units. That lets operators handle unusual workpieces, thin-walled castings, or tight deadlines without constant adjustment. For odd geometries, custom fixtures and adjustable rotation speeds prevent distortion while keeping coverage uniform. Before visiting any production facility, ask whether you can see machines mid-assembly, view test reports, and check spare parts stock. After delivery, the relationship should continue with fast wear-part supply, remote support, and scheduled follow-ups aimed at improving cycle times and reducing waste. A genuine factory treats the sale as the start of ongoing refinement, not the end of the conversation.
Contact Us
Contact Person: Bruce
Email: [email protected]
Tel/WhatsApp: +86 15166629468
Website: https://www.povalchina.com/